How Automation Improves Precision in Rubber Molding Operations
Anyone who has spent time around a rubber press knows the frustration. Same compound, same mold, same crew, and still one batch comes out with thick flash while the next has a void near the edge. Rubber is not a forgiving material. A lot of what goes wrong on the shop floor comes from small variations that nobody caught in time.
This post looks at where those variations come from and how automation reduces them. It also covers where pneumatic components fit in, because many of the repetitive motions on a molding line (pushing, clamping, lifting, ejecting) are exactly the kind of work compressed air is used for.
Where precision gets lost in rubber molding
Most rubber parts are made by compression, transfer or injection molding. Each has its own weak spots.
In compression molding, an uncured piece of compound called a preform is placed in a heated mold cavity and pressed into shape. One engineering guide describes this process as producing parts of “intermediate precision”, meaning parts that meet standards such as RMA-A2 and RMA Class A O-ring tolerances [1]. The same guide points out that the preform itself needs a tolerance on size and shape. Too much material is wasteful and makes the flash thick, while too little can leave voids in the part [1].
That preform step is a common source of trouble. A rubber molder’s process guide calls preform production a labor-intensive step that can affect the finished product through variability in preform weight and shape [2]. Transfer molding also needs preforms, and the same source lists increased waste or excess flash as its main disadvantage [2].
There is a wider pattern here too. One published study on robotic automation describes rubber mixing and molding as traditionally labor-intensive and highly sensitive to process variability [7]. In other words, the more a result depends on someone’s hands and judgment at every cycle, the more the result drifts.
Four places automation makes a real difference
1. Dosing the right amount of material
The most direct fix for preform variation is to stop relying on eyeballed or hand-cut pieces. A US patent on automated rubber molding describes a dispenser that places rubber pellets into the mold cavity in predetermined amounts, at chosen locations. The amount can be set by weight, volume or dispensing time, and the patent says dispensing by weight can be preferable [6].
Injection molding goes a step further. Rubber injection molding began in the mid-1960s, adapted from the plastics process, and because it does not use preforms, nobody has to place them in a cavity or pot by hand [2]. For liquid silicone rubber, the process uses a metering section, and the cold runner means very little material is lost during injection [3].
2. Holding temperature, pressure and time steady
Rubber cures under heat and pressure, so those two numbers, plus time, decide a lot. Production compression presses typically use a programmable logic controller to monitor and control temperature, pressure and time so that molding stays inside a set tolerance window [1].
The reason this matters is that the variables affect each other. A patent describing injection molding control lists material type, cycle time, shot size, melt viscosity, temperature consistency, clamp pressure and injection pressure among the interrelated parameters that a control system has to handle. It also notes a trend toward fewer operators watching each machine, which calls for more automatic control [4].
A research paper on injection moulding control adds a useful detail: the pressure profile during the injection and packing phases directly affects the quality of the finished part [5]. That paper deals with thermoplastics, not rubber, so treat it as an illustration of the principle and not as rubber-specific data. The takeaway is simple, though. If a variable has a direct effect on quality, it is better to measure and control it every cycle than to check it now and then.
3. Handling parts the same way every time
Opening the mold, taking out the part and clearing the cavity is where hand-to-hand differences show up. If an operator pulls a part a little slowly one time and quickly the next, or leaves a bit of flash behind, the next cycle starts from a different place.
The same automated molding patent covers de-molding as well. It describes placing a tab on the part in an area likely to carry flash, so the tab can be removed in the same step as de-flashing [6]. That is a small design choice, but it shows how automation planning reaches past the press itself.
Ejection is another repeatable motion. In injection molding machines, ejector pins can be driven forward by a pneumatic cylinder, a linear motor or a servomotor [9]. Which one is right depends on the speed, force and position control the job needs.
4. Cutting out manual variation across the whole line
A study of industrial robots in rubber mixing and molding reports findings that automation reduces cycle times, improves compound homogeneity and mold precision, and lowers defect rates [7]. It is one study, and results will differ from plant to plant, so it is better read as a direction than a promise. I have left out any specific percentages because they depend on the plant and the part.
What “precise” means to your customer
Customers rarely ask how a part was made. They ask whether it fits. For molded rubber, tolerance classes are set out in ISO 3302-1, which specifies dimensional tolerance classes and values for moulded, extruded and calendered solid rubber products. It does not apply to precision toroidal sealing rings [8].
Automation does not change those tolerance classes. What it does is make it easier to stay inside them from the first part to the ten-thousandth, because the weight, the pressure, the timing and the handling stop changing with every cycle. That is a conclusion drawn from the sources above and not a figure from the standard itself.
Where pneumatics fits into an automated molding line
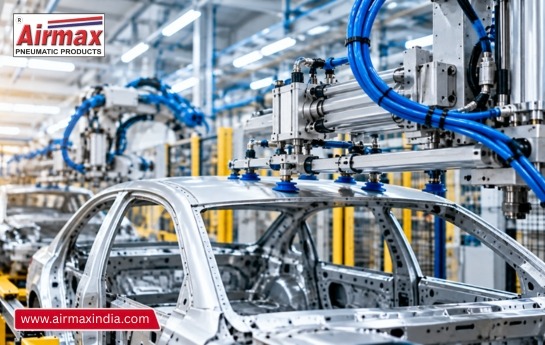
A molding line has plenty of short, fast, repeated movements. Pushing a part out, closing a guard, lifting a tray, holding a fixture. Compressed air is a common way to do these, and the parts involved are fairly standard:
- Actuators. A pneumatic cylinder turns air pressure into a straight push or pull. Our double acting cylinders are powered in both directions.
- Valves. A directional control valve decides where the air goes and when. If a machine controller sends a signal, a poppet solenoid valve is one way that signal becomes motion.
- Air preparation. FRL units filter, regulate and lubricate the air, and moisture separators take water out of the line.
- Fittings and tubing. Pneumatic accessories connect everything, and loose or leaking connections affect repeatability.
A cylinder is only as repeatable as the air that feeds it. If pressure wanders or the air is wet, the same motion will take a slightly different time on each cycle. That is why air preparation and upkeep deserve as much attention as the cylinder itself. Our posts on a pneumatic system preventive maintenance checklist and on finding and fixing compressed air leaks cover the basics.
Pneumatics is not the answer to everything. Where a motion needs very fine position control or high force, electric or hydraulic drives may be a better choice. If you are weighing the options, our pneumatic vs hydraulic comparison lays out the trade-offs.
Where to start if you are automating a rubber molding line
You do not need to automate everything at once. A sensible order looks like this:
- Fix the material first. Weigh preforms or switch to metered dosing before touching anything else. Material quantity is the easiest variable to get wrong.
- Record the cure variables. Log temperature, pressure and time for every cycle. You cannot control what you do not measure.
- Automate the repeated handoffs. Part ejection, tray movement and guard operation are good candidates because the motion is the same every time.
- Look after the air supply. Check filters, regulators and leaks on a schedule.
It is also worth saying what automation will not do. It will not rescue a poorly mixed compound or a worn mold. It makes a good process repeatable, and it makes a bad process repeat its mistakes faster.
Talk to us about your application
Airmax Pneumatics Ltd has manufactured pneumatic valves and related products in Ahmedabad since 1992, and our products carry ISO and CE certifications (see our certificates page). If you are planning an automated line and want to talk through cylinders, valves or air preparation, you can contact our team or download the product catalogue.
References
- Apple Rubber. “Hot Topics for Engineers.” https://www.applerubber.com/hot-topics-for-engineers/?p=742
- Timco Rubber. “Rubber Injection and Transfer Molding Process.” https://timcorubber.com/rubber-resources/rubber-molding-process
- Wikipedia. “Injection molding of liquid silicone rubber.” https://en.wikipedia.org/wiki/Injection_molding_of_liquid_silicone_rubber
- US Patent 4,767,579. “Method of precision volumetric control of a moldable material in an injection molding process.” https://image-ppubs.uspto.gov/dirsearch-public/print/downloadPdf/4767579
- “Model-based pressure tracking using a feedback linearisation technique in thermoplastic injection moulding.” arXiv:2403.04388. https://arxiv.org/pdf/2403.04388
- US Patent Application 2017/0113379. “Automated Rubber Molding and De-molding.” https://patents.justia.com/patent/20170113379
- “Automation of Rubber Mixing and Molding Processes Using Industrial Robotics for Productivity Optimization.” ResearchGate. https://www.researchgate.net/publication/401278609_Automation_of_Rubber_Mixing_and_Molding_Processes_Using_Industrial_Robotics_for_Productivity_Optimization
- ISO 3302-1:2014. “Rubber — Tolerances for products — Part 1: Dimensional tolerances.” Standards Council of Canada listing. https://scc-ccn.ca/standardsdb/standards/8155147
- US Patent 7,275,922. “Controller for an ejector mechanism in an injection molding machine.” https://image-ppubs.uspto.gov/dirsearch-public/print/downloadPdf/7275922